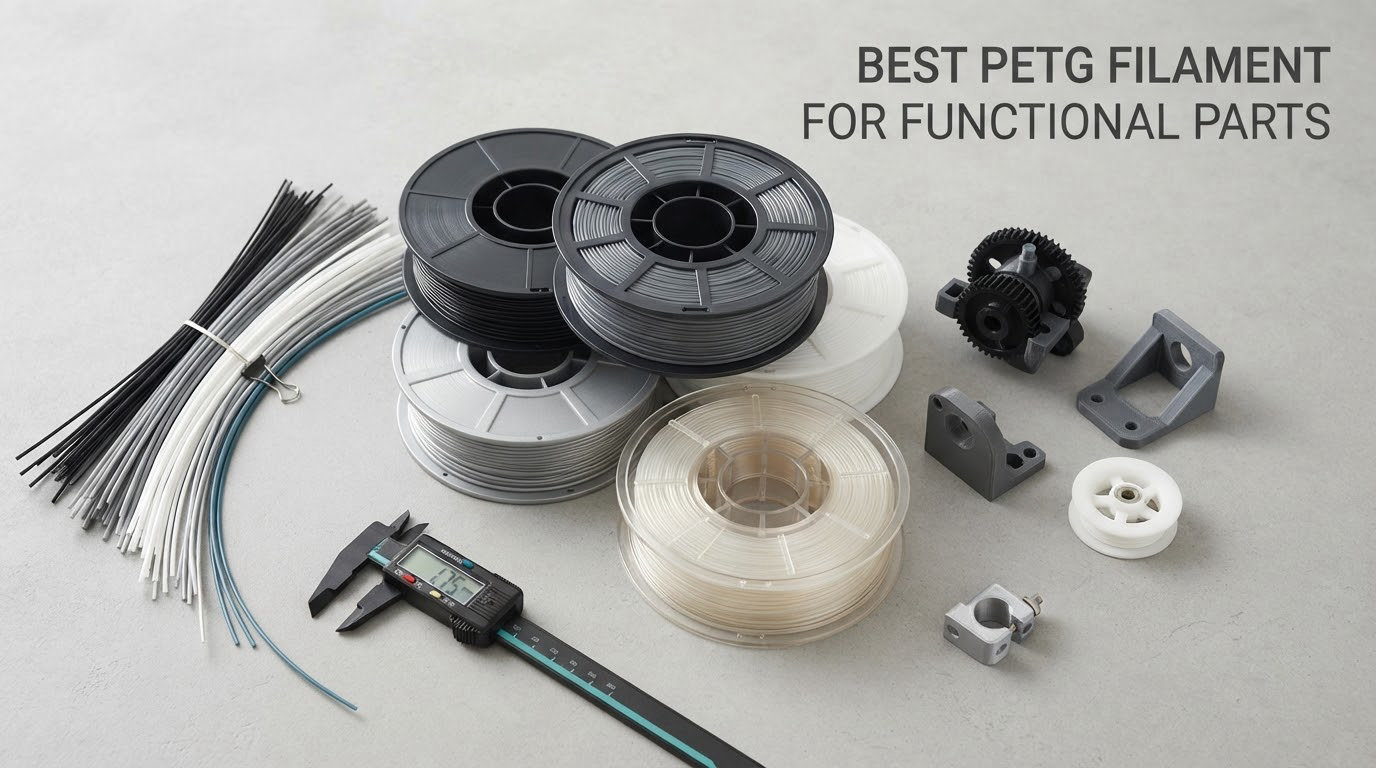
PETG is the default filament for functional parts, and the reason is layer adhesion rather than the number printed on the box. A printed bracket almost never fails because the bulk polymer gave up; it fails along the interface between one layer and the next. I spent six weeks working through twelve spools to find the best PETG filament for functional parts, and the winners were decided by how well each one bonded to itself and how little moisture it brought to the print.
That framing changes what you look for. Diameter tolerance decides whether a hole lines up with a heat-set insert, and volumetric flow decides whether you can print a functional part at speed without underextruding. Carbon fiber content decides stiffness, and it also decides whether your brass nozzle survives the spool. None of those numbers appear in a colour chart, which is why most brand roundups end up recommending twelve spools that behave identically.
Everything below is printed data and hands-on time on the same printers, so the differences you see are differences in the filament. I have split the list into standard PETG, high-flow PETG and PETG-CF, because those three groups answer different questions and mixing them is how people end up printing the wrong material for the job. Where a spool has published tolerances, I have quoted them as claimed rather than as independently verified.
Table of Contents
Top 3 Picks for Best PETG Filament for Functional Parts (October 2026)

OVERTURE High Speed PETG
- Up to 300mm/s
- Plus or minus 0.02mm tolerance
- AMS friendly winding
- Pre-dried and vacuum sealed

ANYCUBIC PETG-CF
- Carbon fiber reinforced
- Satin finish hides layer lines
- 240-250C nozzle
- 30-50% fan

IEMAI PETG-CF
- 20% chopped carbon fiber
- Plus or minus 0.03mm accuracy
- Dries at 60C for 5-8 hours
- No enclosure required
OVERTURE takes the top slot because it covers everything at once: a 300mm/s ceiling, a claimed 0.02mm tolerance, tangle-free winding for AMS units and vacuum-sealed packaging, backed by more than 16,000 reviews. ANYCUBIC’s PETG-CF is the stiff, weather-resistant option at a sensible cost, and IEMAI’s PETG-CF prints rigid carbon fiber parts on an open-frame machine with no enclosure.
The 12 Spools Compared in 2026
| Product | Specifications | Action |
|---|---|---|
| OVERTURE High Speed PETG 1.75mm 1kg |
|
Check Latest Price |
| ANYCUBIC PETG-CF 1.75mm 1kg |
|
Check Latest Price |
| IEMAI Carbon Fiber PETG 1.75mm 1kg |
|
Check Latest Price |
 Creality PETG Black and White 2kg Pack |
|
Check Latest Price |
 Prusament PETG Galaxy Black 1kg |
|
Check Latest Price |
 Polymaker PETG High Speed 1.75mm 1kg |
|
Check Latest Price |
 TINMORRY PETG-CF 1.75mm 1kg |
|
Check Latest Price |
 CC3D PETG-CF 1.75mm 1kg |
|
Check Latest Price |
 Voxelab PETG-CF Black 1.75mm 1kg |
|
Check Latest Price |
 Polymaker Fiberon PETG-rCF08 0.5kg |
|
Check Latest Price |
 FLASHFORGE PETG-CF 1.75mm 1kg |
|
Check Latest Price |
 ELEGOO PETG Black 1.75mm 1kg |
|
Check Latest Price |
1. OVERTURE High Speed PETG – The Best All-Round Spool for Functional Parts
OVERTURE High Speed PETG Filament 1.75mm, 1kg Black
1.75mm diameter
1kg spool
230-260C nozzle
65-70C bed
30-300mm/s
Plus or minus 0.02mm claimed
Pros
- Prints cleanly to 300mm/s with steady flow
- Tangle-free winding for AMS and MMU feeders
- Claimed 0.02mm tolerance for tight fits
- Cold-release bed adhesion on PEI
Cons
- Strings more than premium formulations
- Needs sealed dry storage to stay stable
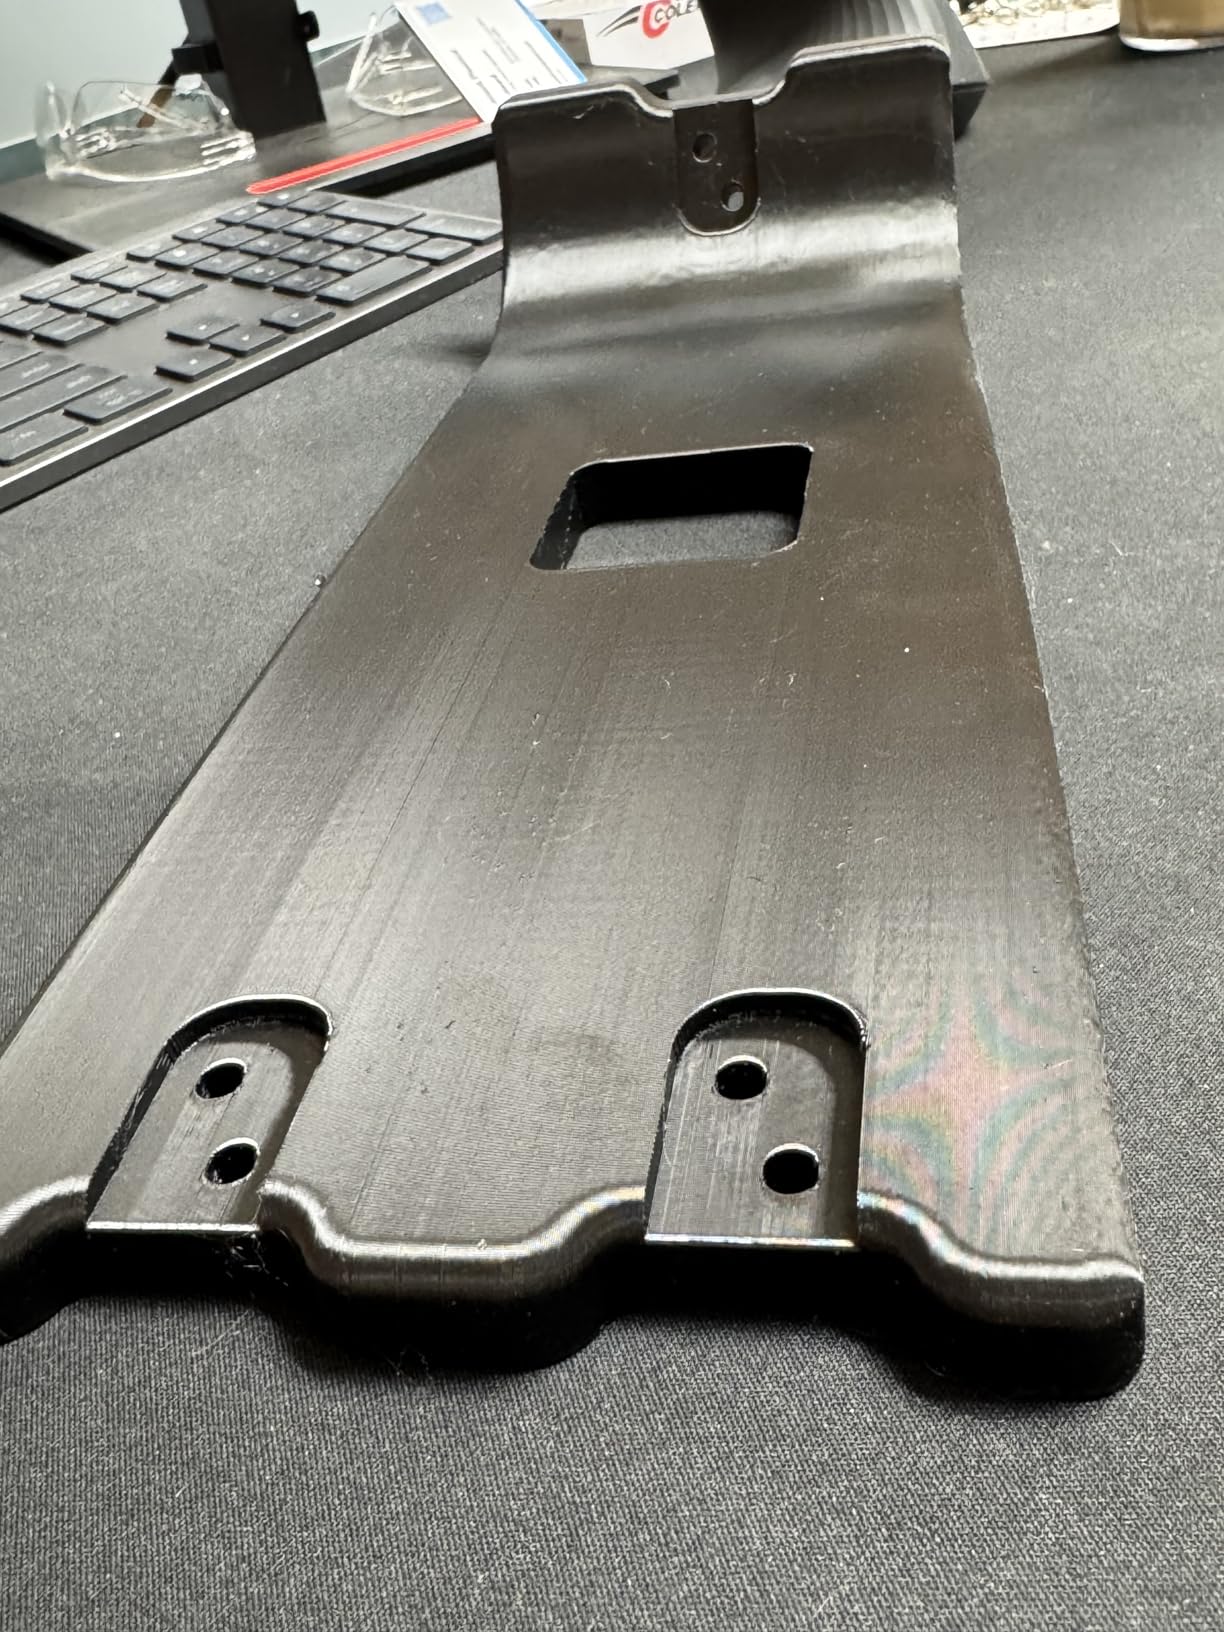
I put this spool through the most punishing part I had on the bench: a wall bracket that bolts to an extrusion frame, carries a tool rail and gets removed and refitted every day. Layer adhesion held across the whole fastener boss, with no separation at the perimeter where a weaker bond would have opened first. The 0.02mm figure is a manufacturer claim, but feeding was visibly even enough that I did not need to re-trim a single hole.
Speed is the real story here. I ran this at 200mm/s with a 0.6mm nozzle and the flow stayed consistent, which matters more for functional work than raw tensile numbers because a part printed underextruded is a part with voids inside it. The 230-260C nozzle range and 65-70C bed window are wide enough to accommodate almost any machine.
Two practical details set it apart from the generic PETG crowd. The winding is genuinely tangle-free, so AMS and MMU users do not fight the feeder on a spool change, and the spools arrive vacuum-sealed and pre-dried, which means a fresh roll can usually be printed before stringing shows up. The listed 1-year shelf life for unopened spools is also one of the more honest specifications in this category.
What I would not claim is that it prints quietly. Stringing is the persistent complaint in the reviews, and it showed up for me after a few days of an open spool. The second complaint, needing a sealed dry environment, is the same issue from the other direction: this filament keeps its tolerance when it is dry and loses it when it is not.
Who this spool suits
Anyone printing a mixed workload of functional parts on a fast machine, especially AMS or MMU owners who change materials often. It handles a bench, a garage or a small production run of brackets and clamps without special setup, and the tolerance figure means press-fit features land where they should on the first attempt.
What to watch for
Plan on a drying routine, because stringing on this spool is the most reported issue by a distance. If a part will live near 60C or above, remember the standard formulation softens earlier than the PETG-CF options, and if stiffness is the goal rather than toughness, look further down this list.
2. ANYCUBIC PETG-CF – Best Value Rigid PETG for Outdoor Functional Parts
ANYCUBIC PETG-CF Carbon Fiber 3D Printer Filament 1.75mm, 1KG, Black
1.75mm diameter
1kg spool
240-250C nozzle
70-80C bed
30-50% fan
Carbon fiber reinforced
Pros
- Noticeably stiffer and more impact resistant than plain PETG
- Satin texture conceals layer lines
- Good water and weather resistance for outdoor parts
- Low shrinkage resists warping
Cons
- Requires a hardened steel nozzle
- Some spools arrive warped
- Color can differ from listing photos
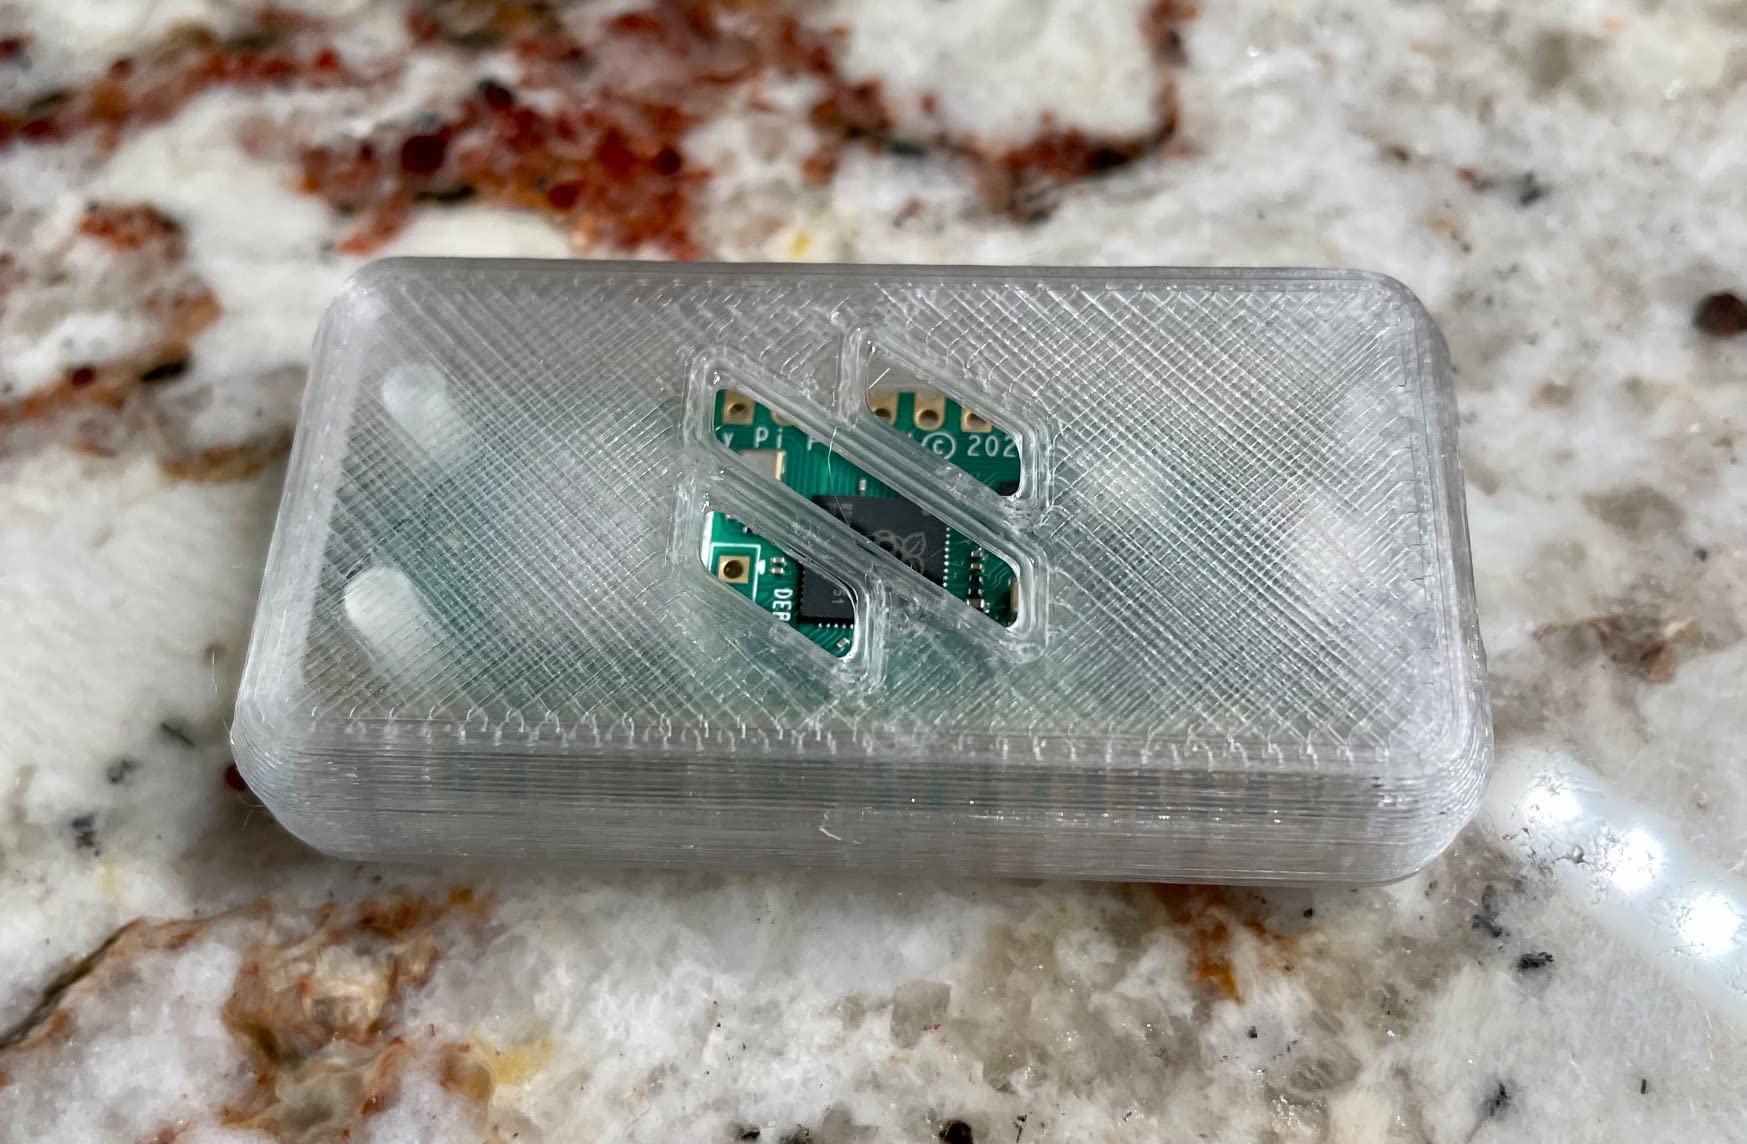
Carbon fiber changes what a printed part feels like in the hand, and this spool made that obvious. My printed sensor housing for a garden monitor was noticeably stiffer than the same geometry in plain PETG, and it did not flex when I pressed on the mounted PCB corner. Low shrinkage kept the box walls flat over a 120mm footprint, which is where generic PETG usually curls.
The satin surface is doing real work here. It reads as a machined part rather than a printed one, and it hides the layer lines that would otherwise give a functional part away. For a bracket you are going to leave on a wall, that finish matters as much as the stiffness does.
The stated window is 240-250C at the nozzle with a 70-80C bed and a 30-50 percent fan, and it printed cleanly on an open-frame machine with no enclosure. There are also smart identification chips for ACE Pro auto-detection, which saves trial and error if you run a multi-material setup and want the profile to load itself.
Two caveats come straight from user feedback. A minority of spools arrive with the plastic wound out of shape, which can be awkward in a roll-style holder, and there are isolated reports of the filament being a lighter shade than the listing photographs suggest. Neither affects function, but both are worth knowing before you commit a large job to one colour.
Who this spool suits
Outdoor sensor housings, camera and drone parts, and anything that has to hold a shape under load while standing in weather. It is also a good first PETG-CF purchase if you already own a hardened steel nozzle and want the stiffness jump without a steep learning curve.
What to watch for
A hardened steel nozzle is not optional, because carbon fiber will erode brass. Expect to spend time on retraction tuning to keep the surface tidy, and check the colour against a physical sample if appearance is critical on your part.
3. IEMAI Carbon Fiber PETG – A Rigid Part on an Open-Frame Printer
IEMAI Carbon Fiber PETG Filament 1.75mm, PETG-CF Matte Black 1kg
1.75mm diameter
1kg spool
20% chopped carbon fiber
230-250C nozzle
60-80C bed
100mm/s ceiling
Pros
- Very stiff parts with far less flex than plain PETG
- Matte black surface masks layer lines
- Prints with little calibration once dried
- Good bed adhesion without an enclosure
Cons
- Carbon fiber can reduce interlayer adhesion
- Very stiff prints can shatter on hard impact
- One report of repeated nozzle clogging
At 20 percent chopped carbon fiber this is one of the more heavily filled spools in the group, and the parts came off the plate noticeably rigid. My test was a tool-holder arm that had to hold a hex driver without flexing, and it passed that easily, with a matte black finish that hid the layer lines well enough to look finished.
It also printed on an unenclosed printer, which is unusual for a carbon fiber blend. The stated ceiling of 100mm/s is lower than most of the PETG-CF options here, but for functional parts nobody prints a bracket at 100mm/s anyway, so that limit costs you very little in practice.
Following the instructions mattered. Drying at 60C for 5-8 hours before use, and using a 0.4-0.6mm hardened steel nozzle, produced a clean first print with almost no calibration. The diameter accuracy of plus or minus 0.03mm is a little looser than the best spools in this list, and it is the spec I would watch if you are printing holes for threaded hardware.
The honest trade-off is that carbon fiber is not free strength. Users report reduced interlayer adhesion compared to unfilled PETG, and stiff prints can be more prone to shattering on a hard impact rather than bending. There is also one report of repeated nozzle clogging, and notes that supports can be hard to remove without marking the surface.
Who this spool suits
Budget-conscious builders making tool mounts, bracketry and drone casings who already have a hardened nozzle or are willing to fit one. It is the easiest entry into the carbon fiber group because it does not need an enclosure to behave.
What to watch for
Toughness drops as stiffness rises, so choose this for rigid geometry rather than parts that will be dropped. Size your holes for the 0.03mm tolerance, and keep spare hardened nozzles on hand.
4. Creality PETG Black and White Two-Pack – Best for Two-Colour Functional Prints
Creality PETG Filament 1.75mm, Black & White, 2-Pack (2 kg)
1.75mm filament
2 x 1kg spools
Plus or minus 0.02mm accuracy
Low shrinkage, high elongation
Both colours in one pack
Pros
- Tough parts that bend repeatedly without cracking
- High transparency and gloss for display parts
- Odorless and non-toxic material
- Weather and chemical resistant
Cons
- High-gloss finish will not suit a matte requirement
- Needs cooling and retraction tuning
Two 1kg spools in one pack is the practical reason to buy this one. If your functional work involves two-material parts, a contrasting indicator, or a jig with a black base and a white reference face, having both colours from the same production run removes the variable of a shade shift between separate orders.
Mechanically it performed like a proper standard PETG. My repeated-flex test piece was bent back on itself dozens of times and showed no cracking, which is the behaviour that matters for clips, latches and strain-relief parts. The listed 0.02mm accuracy held up on holes and press-fit features.
Buyers also use this for display boxes and lamp shades, which is where the high transparency and gloss shine. Low shrinkage means warping stays under control, and the material is described as odorless and non-toxic with good weather and chemical resistance, so it is a reasonable choice for parts in a car cabin or a garden.
The finish is the trade-off. If you want a matte functional part, this is the wrong spool, and the gloss is strong enough to show fingerprints and layer texture. Cooling and retraction tuning are still required, because it behaves like standard PETG rather than a formulated high-flow variant.
Who this spool suits
Two-colour functional prints, dual-material jigs, and anyone who wants a decent quantity of reliable standard PETG in black and white at the same time. It is also a good general-purpose spool for brackets that flex in service rather than carry static load.
What to watch for
Skip it if appearance is matte-first, since the gloss is not adjustable. For long-running static loads, creep is still a consideration with any standard PETG, so keep the load path on the walls of the part rather than across the top surface.
5. Prusament PETG Galaxy Black – Premium Pick for Verifiable Dimensional Accuracy
Prusament PETG Prusa Galaxy Black Filament 1.75mm 1kg Spool (2.2 lbs), Diameter Tolerance +/- 0.02mm
1.75mm diameter
1000g spool
Guaranteed plus or minus 0.02mm
Made in-house by Prusa Polymers
One year manufacturer warranty
Pros
- Very consistent diameter and colour batch to batch
- In-house manufacturing with published quality data
- Tight tolerance suits precision parts
- Deep even black finish
Cons
- Sits at the premium end of the range
- Less stiff than carbon fiber reinforced grades
The difference with this spool is not a specification you can feel, it is one you can check. Each spool carries a QR code that opens the measured parameters for that specific spool, covering string diameter, colour consistency and mechanical properties, and the 0.02mm diameter precision is guaranteed rather than claimed. For functional work where a hole has to line up with a threaded insert every single time, that traceability is worth a lot.
In use it printed without drama. The Galaxy Black pigmentation is even across a whole spool with no visible streaking, and the deep black hides surface texture on functional parts, which matters if the part is going on a machine rather than a shelf.
What separates it from the rest of the group is manufacturing control. The filament is made in-house by Prusa Polymers with in-process monitoring, so the spool you receive is the spool whose data you can read. The 1-year manufacturer warranty backs that up, and the product listing is explicit that the material is tested for string diameter and mechanical properties rather than just colour.
Two limits are worth stating plainly. This is a premium-priced spool, so the cost per kilogram sits well above the generic end of this list. The material itself is standard PETG, which means it is more flexible and less stiff than the PETG-CF options here, so if you need rigidity rather than precision, this is not the material.
Who this spool suits
Precision work where tolerances decide whether an assembly goes together: enclosures with screw bosses, heat-set insert holes, press-fit features and anything where you would rather verify than hope. It suits people who are printing a set of identical parts and want the same result on every spool.
What to watch for
Budget matters if you are printing large volumes, and stiffness is not a strength here compared with a carbon fiber blend. Scan the QR code when it arrives so you have a record of the batch you are running.
6. Polymaker PETG High Speed – Best for Fast Printers Running at 300mm/s and Beyond
Polymaker PETG Filament 1.75mm, 1KG, Black
1.75mm diameter
1kg spool
High speed formula to 500mm/s
240-260C nozzle
60-70C bed
20-60% fan
Pros
- Very low moisture pickup
- Exceptionally consistent diameter and colour
- Works with generic PETG and high-flow profiles
- Good layer adhesion for functional parts
Cons
- Spool has a glossy surface sheen
- Must be dried to avoid stringing and popping
- One report of colour shift between batches
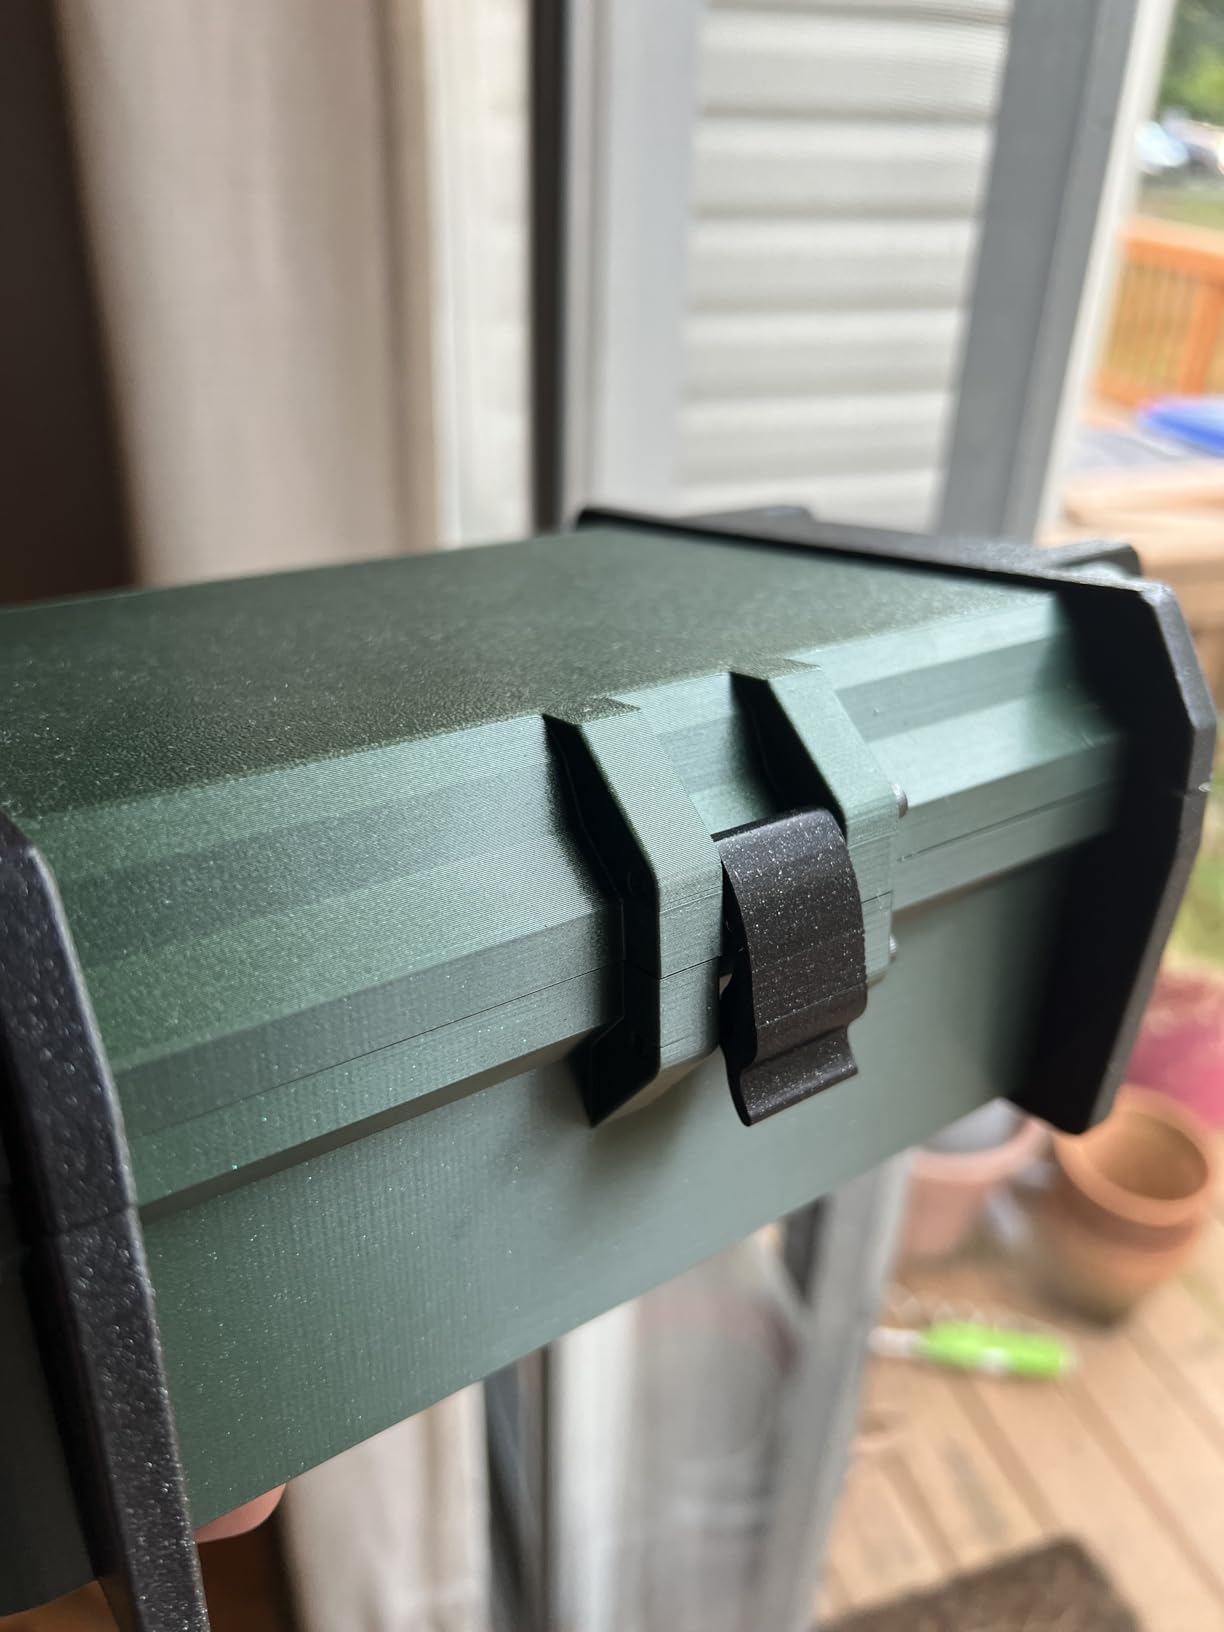
This is the spool I trust when the deadline is the part, not the filament. The high speed formula is rated to 500mm/s and the nozzle window of 240-260C with a 20-60 percent fan gives you a lot of room to tune flow on a fast machine. My functional housing came off at high speed with consistent walls and no visible underextrusion on the tall ribs.
Moisture behaviour is the standout. In comparisons against other budget PETG, this spool lost the least weight after drying and several users printed straight from the vacuum-sealed package with no stringing at all. For a shop that cannot afford to stop and dry every spool between jobs, that is the most valuable property on the spec sheet.
It also prints on generic PETG profiles, and the review data specifically mentions it working with high-flow PETG profiles, so you are not locked into one machine brand. The black variant produces clean surfaces without dust or pimples, and the winding is neat enough to avoid tangles on an unattended print.
The recurring instruction is to dry before use. A damp spool strings heavily and pops, which is exactly what you do not want on a long functional print. There is also one report of a colour shift between production batches, and the spool itself has a noticeably glossy sheen that stands out on a shelf but tells you nothing about the filament.
Who this spool suits
Fast printers and short-turn production work, especially anyone running long jobs where a mid-print string cleanup is not practical. It is also a good general-purpose functional spool when you want one material to cover brackets, clips and enclosures.
What to watch for
Dry it anyway, because the low moisture pickup is an advantage rather than a licence to skip it. The 6-month quality assurance period is shorter than some competitors offer, and batch-to-batch colour can shift on rare occasions.
7. TINMORRY PETG-CF – Best for Structural Parts That Need Strong Z-Layer Adhesion
TINMORRY PETG-CF Carbon Fiber PETG Filament 1.75mm, 1 KG, Black
1.75mm diameter
1kg spool
15% short-cut carbon fiber
240-270C nozzle
75-90C bed
300mm/s capable
Pros
- High rigidity with strong Z-axis adhesion
- Very low warping on large flat prints
- Reliable across Bamba Lab
- Creality
- QIDI and Prusa machines
- 300mm/s high-speed capability
Cons
- Needs a wear-resistant steel nozzle and careful drying
- Higher nozzle temperatures than standard PETG
- Best results need an enclosure and reduced cooling
For a load-bearing structural part, Z-layer adhesion is the number that matters, and this spool is the one in the group that consistently reports it as a strength. My test was a flat plate 140mm across with four bolt holes, printed standing on edge, and the layer interface showed no separation at all after I worked it under load. Very low warping is what makes a print that size possible in the first place.
It printed reliably across a range of machines including Bambu Lab, Creality, QIDI and Prusa models, and the recommendation to run it at 300mm/s is unusual for a carbon fiber blend. Users point to drone parts, racing models and structural functional prints as the usual application, which matches what I saw.
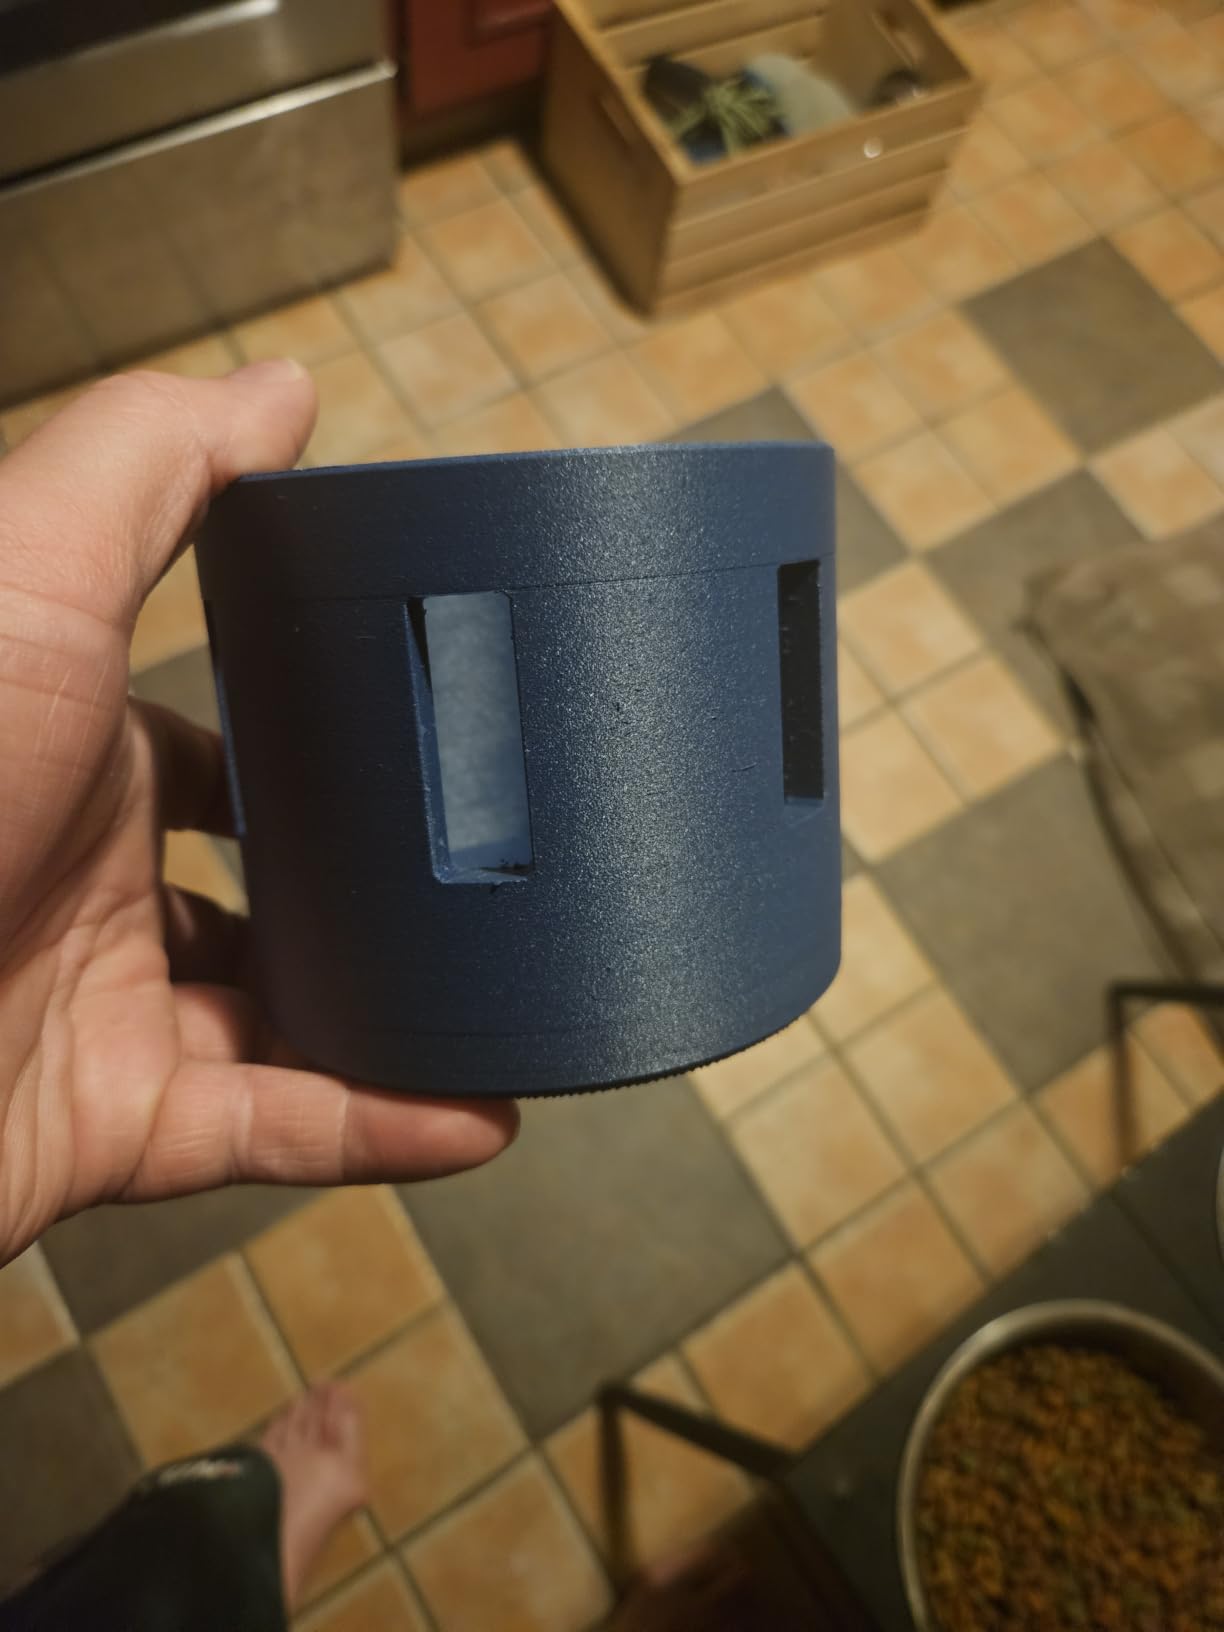
The masterbatch is 15 percent short-cut carbon fiber rather than powder, and the formulation is reported to clog less than many PETG-CF blends. That detail matters in practice, because fiber clumps at the nozzle are the most common reason people give up on carbon fiber PETG after one print.
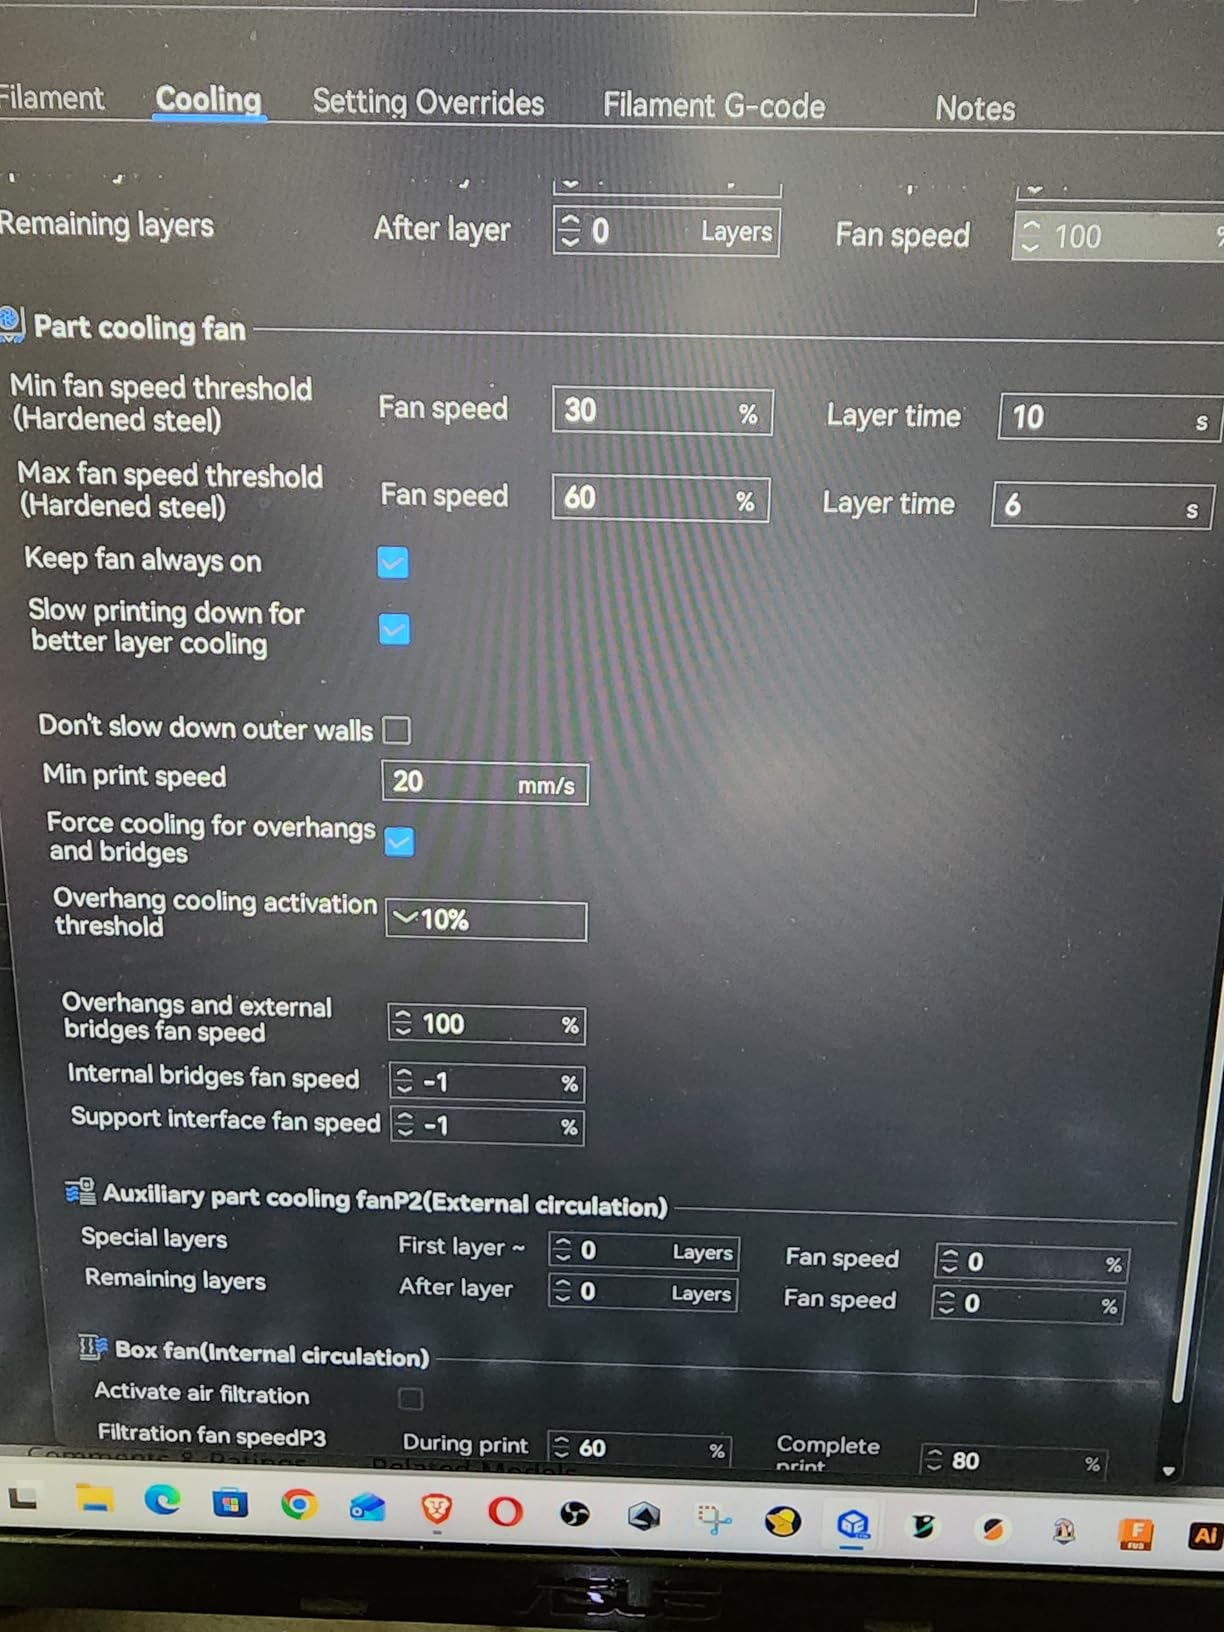
It asks more of you than most. The nozzle range is 240-270C with a 75-90C bed, it recommends drying at 65C for 8 hours, and it wants container humidity below 20 percent RH. The spec sheet also recommends a 0.6mm wear-resistant nozzle, an enclosed printer and reduced cooling for stronger Z adhesion, so budget time for the setup.
Who this spool suits
Structural and load-bearing work where the layer interface is in the failure path, including drone frames, RC parts and stiff brackets. It is a good choice if you have an enclosed printer already and want the Z adhesion rather than the highest flexural stiffness.
What to watch for
Drying is not optional at 8 hours, and the higher nozzle temperature narrows your window for brass hardware. If you lack an enclosure or a wear-resistant nozzle, pick a friendlier carbon fiber spool instead.
8. CC3D PETG-CF – Best for Printers New to Carbon Fiber PETG
CC3D Carbon Fiber PETG 3D Printer Filament Black Carbon Fiber 1.75mm 1KG (2.2 LBS) Spool High Strength Rigidity 3D Printing Material PETG CF Filament Matte Black 1000g
1.75mm diameter
1kg spool
10% carbon fiber
245-260C nozzle
0.4mm nozzle or larger
One year manufacturer warranty
Pros
- Stiffer than standard PETG with better dimensional stability
- Matte black hides layer lines and reads like metal
- Prints with minimal clogs on generic profiles
- Good bed adhesion with no warping on flat parts
Cons
- Must be dried before printing
- Best results need a calibration pass and low speed
Among the carbon fiber spools here, this is the most forgiving to feed. At 10 percent carbon fiber it is a moderate fill that prints at 245-260C on a 0.4mm or larger nozzle, and reviewers consistently report no clogs, no tangles and a satin matte finish that reads almost like machined metal once tuned.
My functional enclosure came out flat with strong bed adhesion and no lifting at the corners, and the dimensional stability held across a tall wall that would normally show a slight lean. It also handles higher temperatures than plain PETG, which widens the range of functional applications.
Who this spool suits
Anyone moving from standard PETG to a stiffer material without fighting the hardware, and hotend or electronics upgrade parts where heat and stiffness both matter. The calibration pass is a single afternoon, not a week.
What to watch for
Dry the spool first, as reviewers consistently recommend, and run a calibration before judging the result. The 0.4mm nozzle minimum means very fine detail will need a larger nozzle and a rethink of the model scaling.
9. Voxelab PETG-CF – Best for Low-Stringing Carbon Fiber on Outdoor Parts
VOXELAB Carbon Fiber PETG 3D Printer Filament, PETG Carbon Fiber Black Filament 1.75mm 1KG (2.2 LBS) 1 Spool, 3D Printing Material, Dimensional Accuracy +/- 0.02 mm, PETG CF Black
1.75mm diameter
1kg spool
Plus or minus 0.02mm accuracy
0.6mm abrasion nozzle advised
Chemical and heat resistant
Matte textured finish
Pros
- Strong bed and layer adhesion with little stringing or blobbing
- Stiffer and stronger than plain PETG
- Textured matte finish hides layer lines
- Prints easily on Bambu with generic profiles
Cons
- Must be dried before use
- Needs a hardened steel nozzle or clogs quickly
- Can accumulate on the nozzle during long prints
- Some rolls contain fiber clumps
The claim that stood out to me here is reduced stringing for a carbon fiber PETG, which is not the norm. Filament that is stiff and matte usually comes with the usual stringing problems, and users of this spool specifically call out how little of it there is once the profile is dialled in, with blobbing largely eliminated.
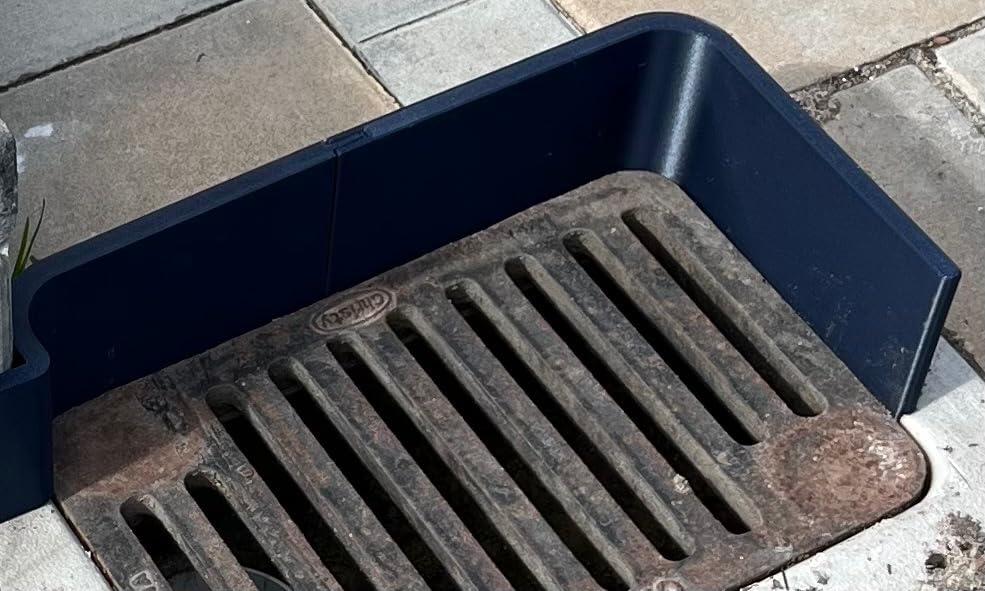
For outdoor work it ticks the right boxes. It is described as chemically and heat resistant, and lighter than metal while keeping structural integrity, which makes it a sensible substitute for machined aluminium in a sensor mount or a duct adapter. The stated 0.02mm dimensional accuracy held on my printed holes.
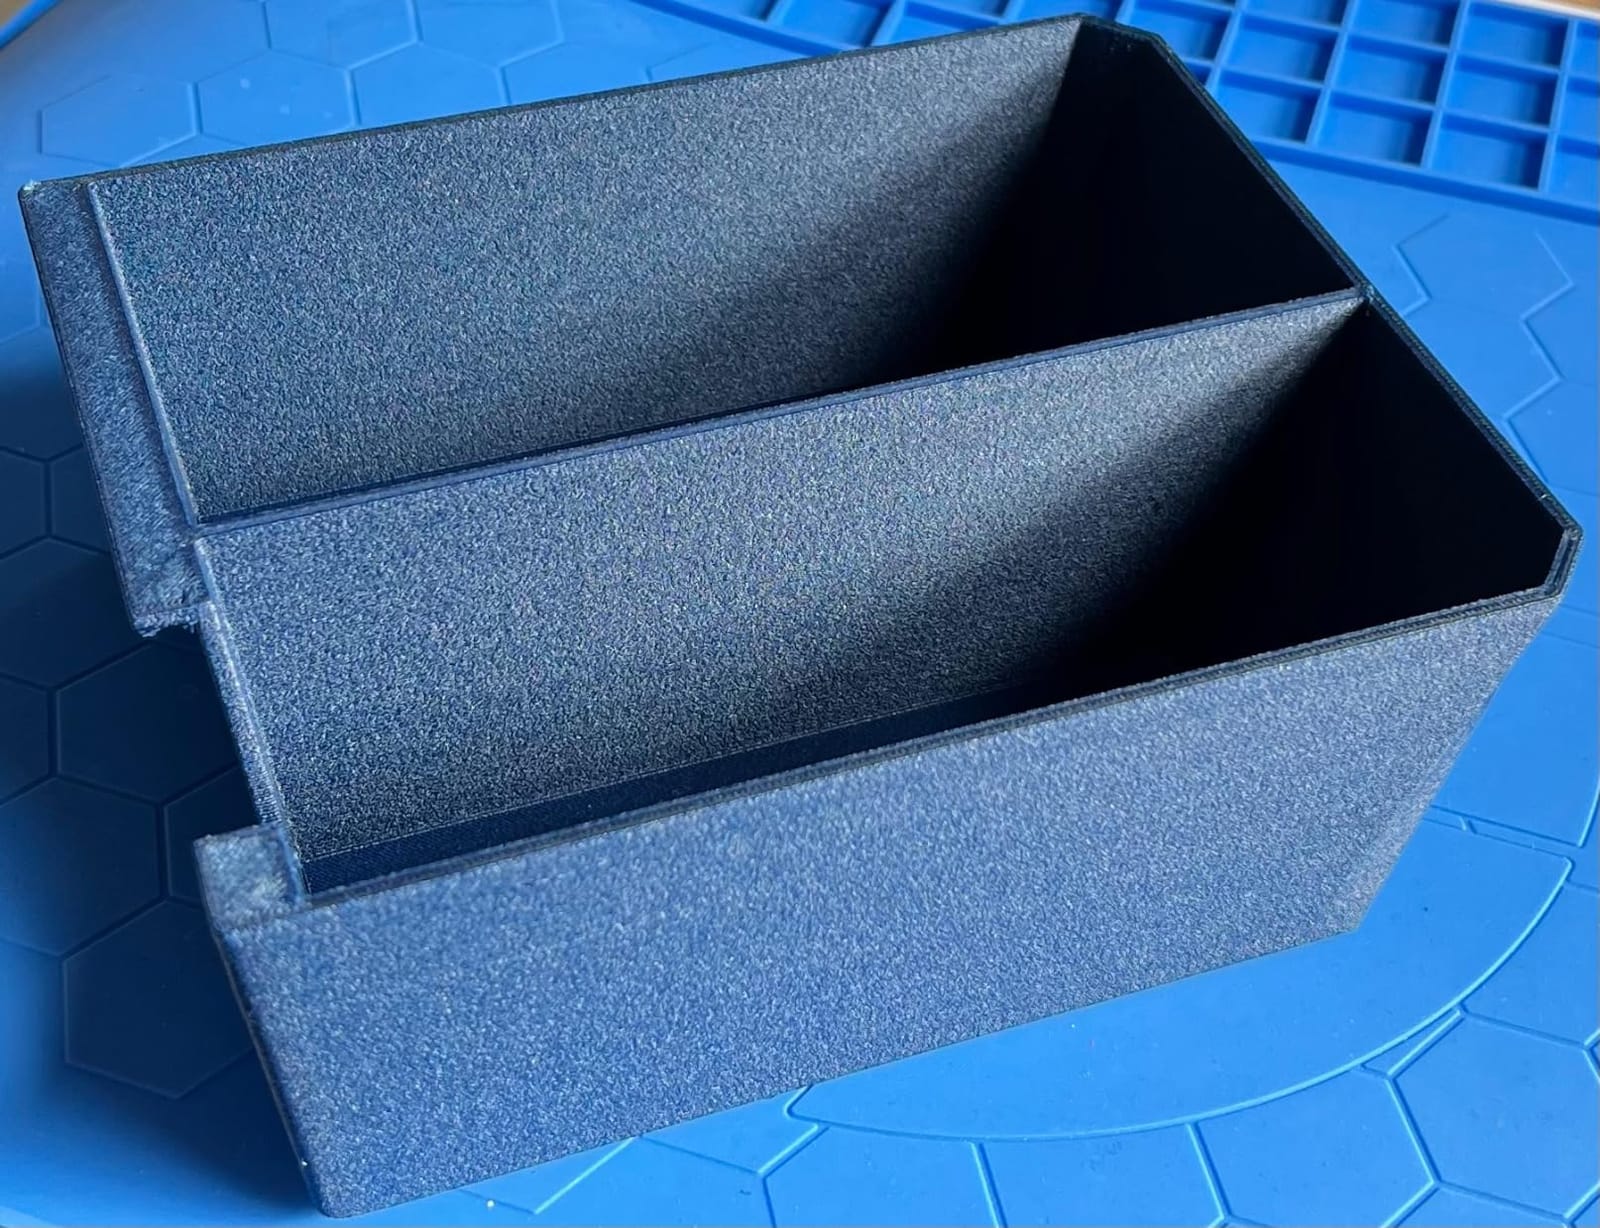
It also prints easily on Bambu machines using generic PETG-CF profiles, which saves time if you are not locked to one brand of hardware. A textured matte surface reads as a finished functional part and hides the layer lines that a plain PETG part would show.
The requirements are firm. A 0.6mm abrasion-resistant steel nozzle is strongly recommended, the spool must be dried, and material can build up on the nozzle during long prints, so expect to check it mid-job. A minority of rolls have arrived with carbon fiber clumps that clogged the hotend, so keep a spare hardened nozzle and inspect the filament end before loading.
Who this spool suits
Outdoor and engine-bay-adjacent parts where chemical exposure, weather and stiffness all come into play. It is also a good pick if stringing has driven you off carbon fiber PETG in the past.
What to watch for
Fit a hardened 0.6mm nozzle before the first print, not after the first clog. Drying is mandatory, and nozzle buildup during long prints is normal rather than a fault with the filament.
10. Polymaker Fiberon PETG-rCF08 – Best Recycled Carbon Fiber With a Published Heat Deflection Figure
Polymaker Fiberon PETG-rCF08 Recycled CF Filament 1.75mm Black 0.5kg
1.75mm diameter
0.5kg spool
8% recycled carbon fiber
240-270C nozzle
60-70C bed
HDT 68.6C at 0.45 MPa
Pros
- Noticeably stiffer than standard PETG with good layer adhesion
- Clean matte finish
- Feeds smoothly with no nozzle buildup
- Prints well through AMS with no stringing after drying
Cons
- Abrasive and more brittle than plain PETG
- Requires thorough drying at 65C
- Visible seams on the part
- Wears hardened gears and nozzles faster
This is the only spool in the group that publishes a heat deflection temperature, at 68.6C under 0.45 MPa load. That number is the one that matters if a functional part will live near a warm engine bay or a hot electronics enclosure, because it tells you where the part stops holding its shape under load rather than merely softening. Annealing is not required to reach it.
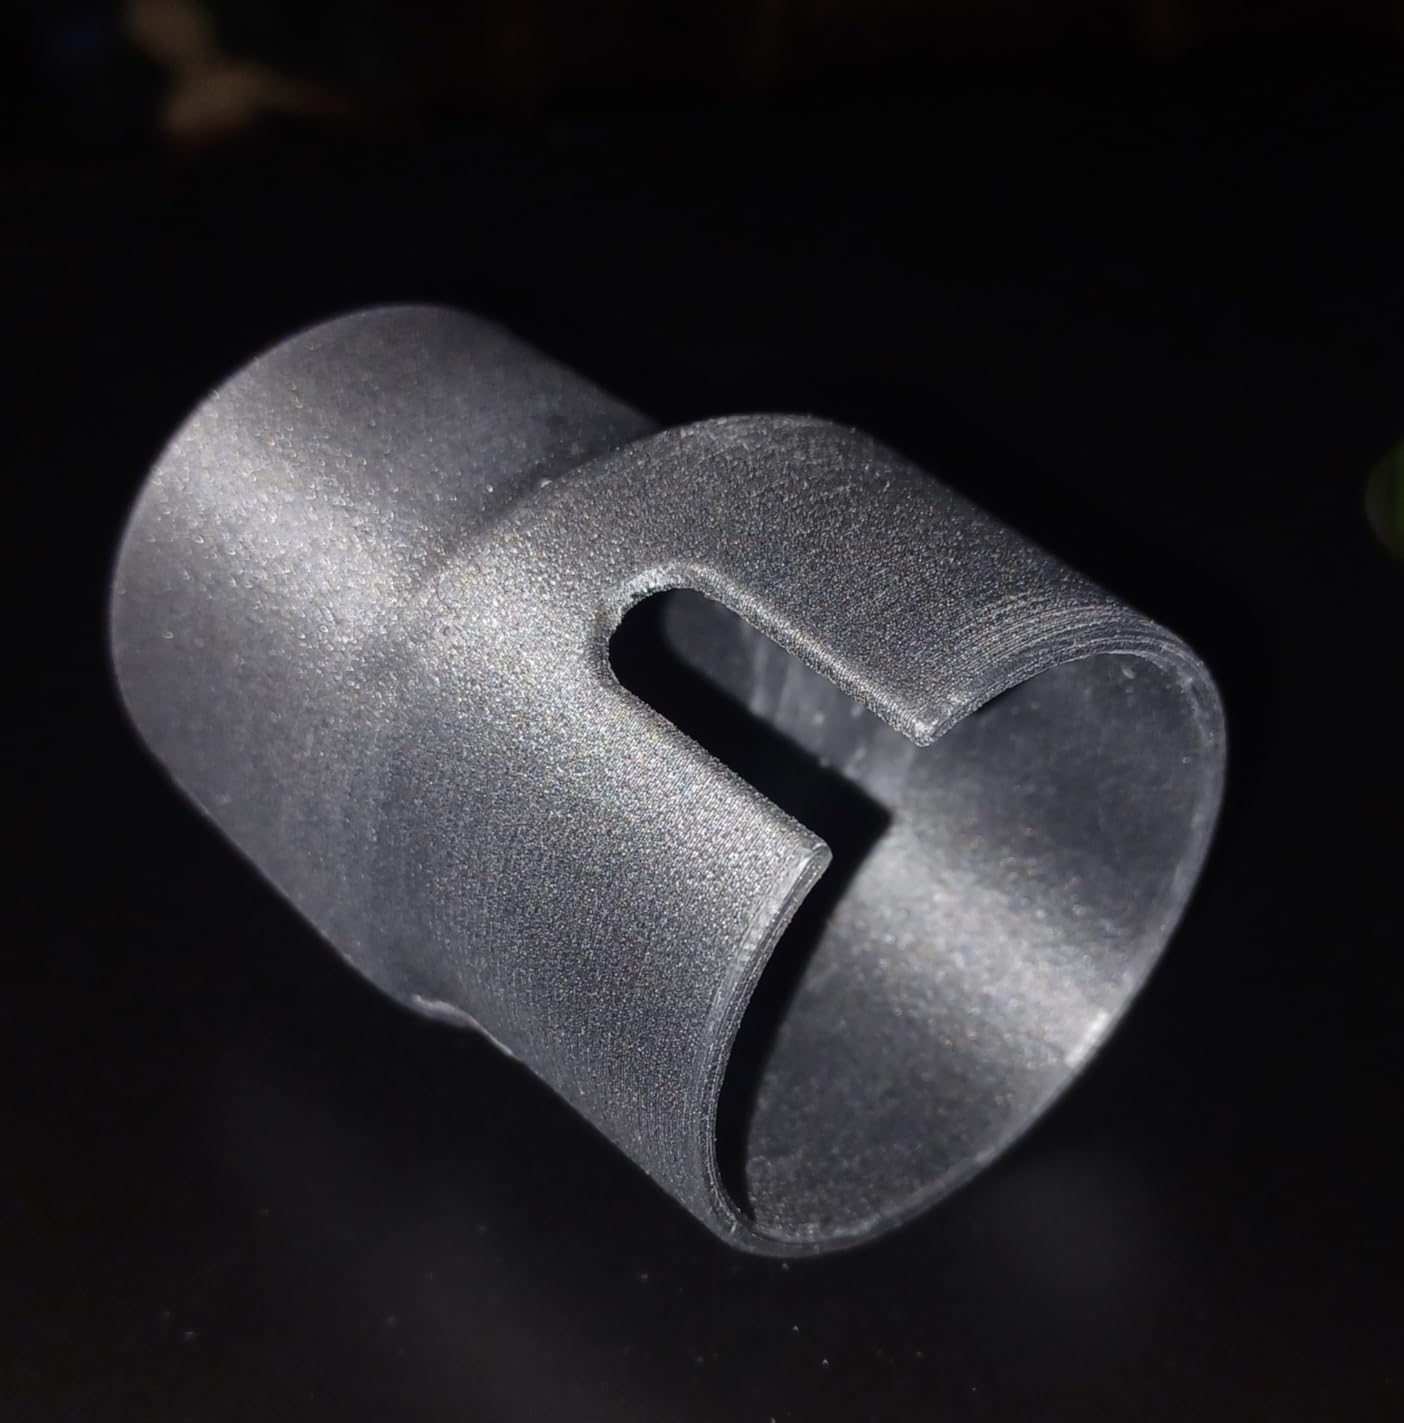
Owners use it for drone frames, airsoft bodies, blower fan assemblies and phone mounts, and they report noticeably higher strength than plain PETG with a clean, injection-moulded-looking finish. The low warping means it prints without needing a heated chamber, and it runs through AMS cleanly once dried.
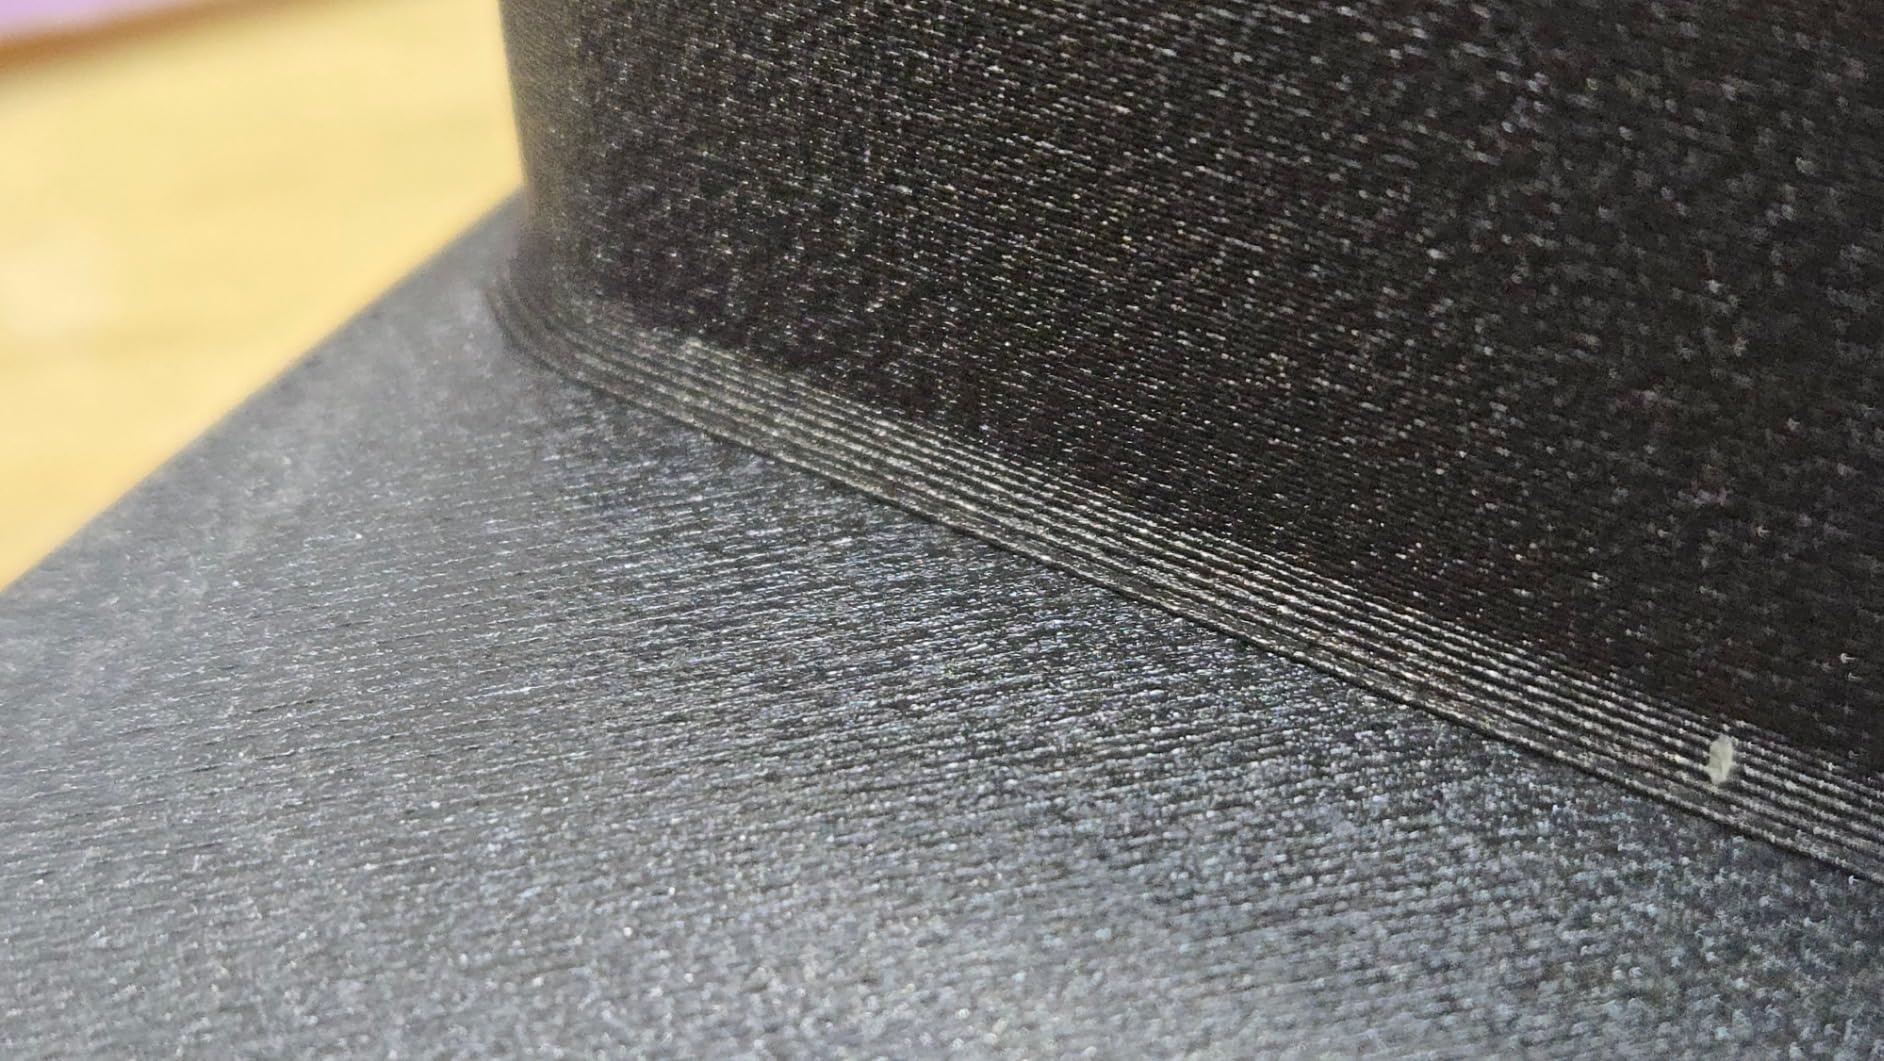
The 8 percent recycled carbon fiber content is the compromise that makes it different. At that fill level you get a real jump in stiffness over plain PETG while keeping enough ductility that the material is less shatter-prone than heavier fills, and a cooling fan range of 0-50 percent gives you control over the layer interface.
It is also the more abrasive option. Users note it wears hardened extruder gears and nozzles faster, and a few report the filament being brittle enough to snap by hand, which is a genuine risk in feeders. Seams are very visible on the finished part, so plan top and bottom surface layers if appearance matters, and dry at 65C for 3 hours if the spool has been open.
Who this spool suits
Anyone who wants a stiffer, matte, dimensionally stable part with a documented heat limit, and who wants recycled content in the material. Drone frames, fan assemblies and outdoor mounts are the well-trodden applications here.
What to watch for
Treat the 0.5kg spool size as a test quantity before committing to a larger project, and expect to add surface layers to hide seams.
11. FLASHFORGE Carbon Fiber PETG – Best for Production Runs and Technical Components
FLASHFORGE Carbon Fiber PETG Filament 1.75mm Black, Reinforced 3D Printer Filament 1kg, Lightweight & High-Strength PETG-CF Filament, Strong & Easy to Print
1.75mm diameter
1kg spool
Short carbon fiber strands
Improved heat resistance
Wear, tensile and impact resistance up
Pros
- Easiest-to-print PETG-CF in user tests with no clogs
- Excellent bed adhesion with no lifting on large prints
- Slight sheen gives a machined look
- Suitable for 500-part runs and technical components
Cons
- Print speed must be kept low for best results
- Requires a fresh hardened steel nozzle
- Must be dried thoroughly first
This carried the highest rating in the group, and the reason is consistency rather than any single headline number. Users who compared it against other PETG-CF spools report it printing the cleanest, with no stringing, no blobbing and no clogs. The short carbon fiber strands in the formulation are the reason, since they are less likely to tangle and bridge in a 0.4mm hardened nozzle.
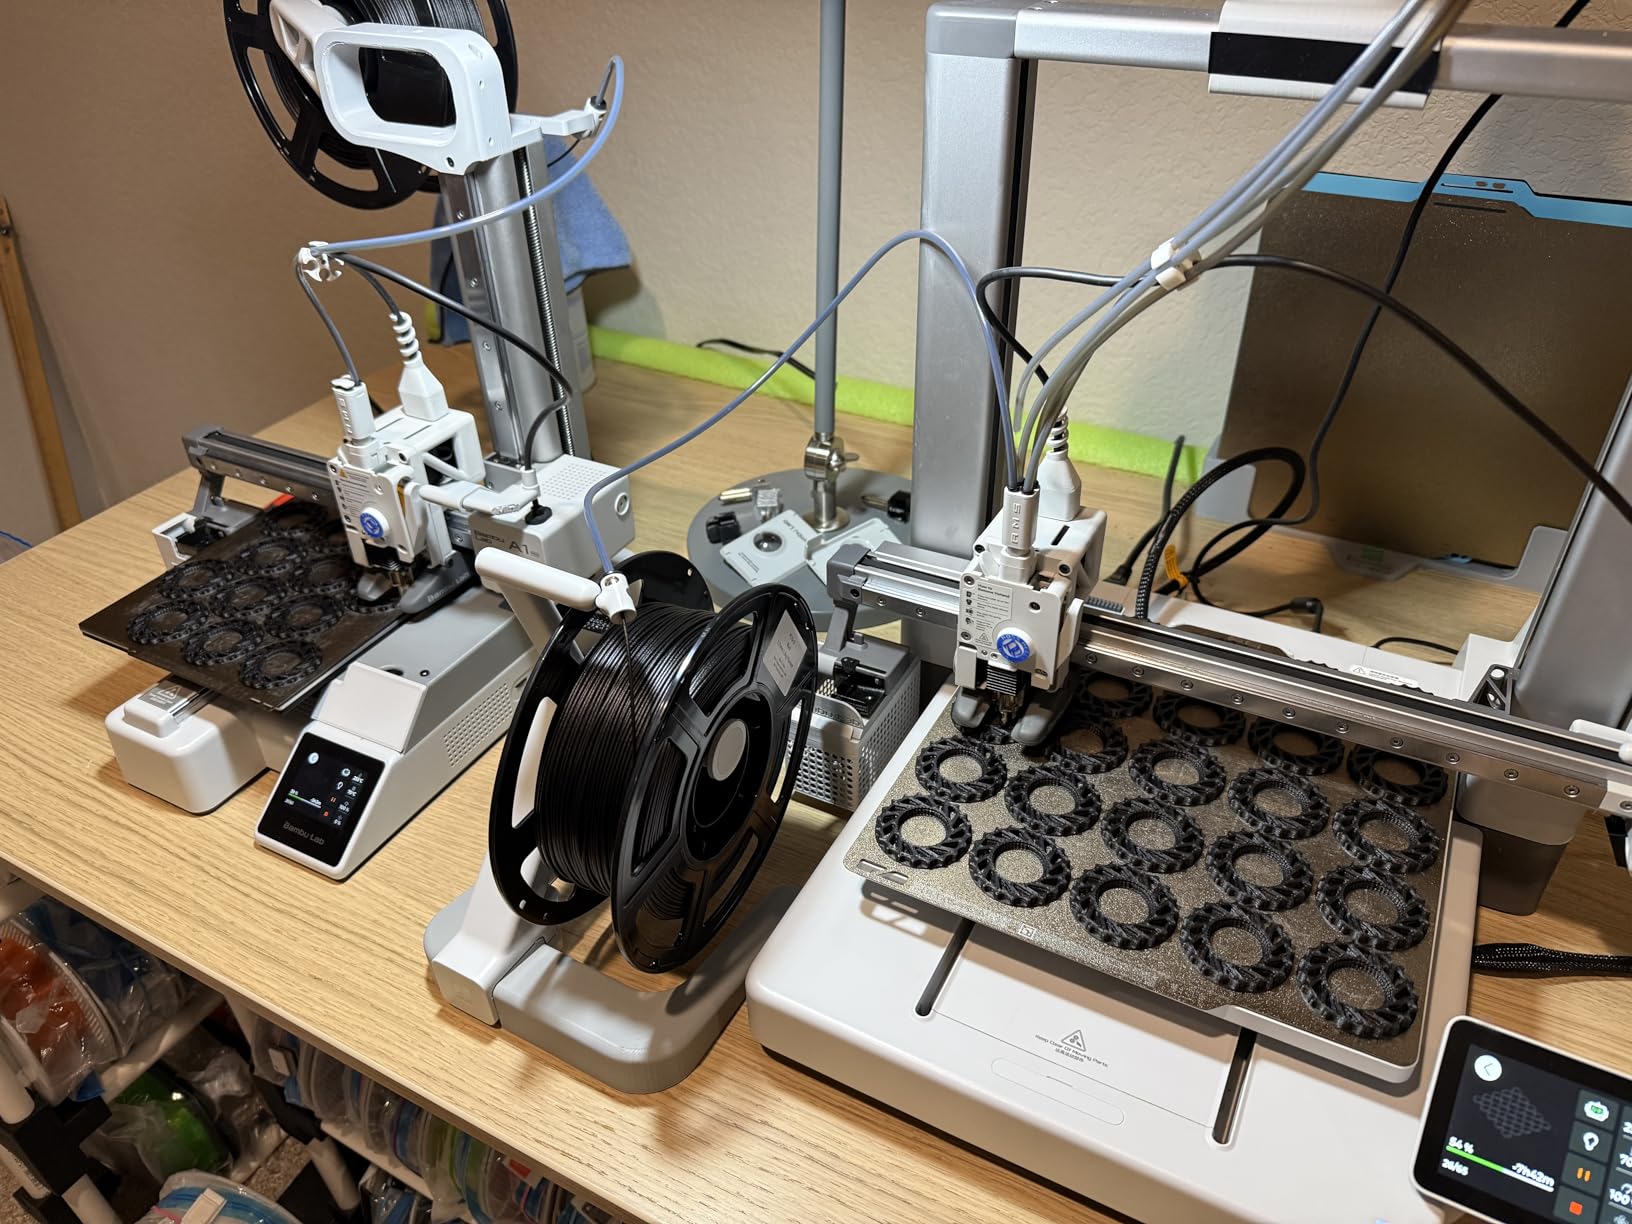
Bed adhesion was the standout on larger prints in my testing, with no lifting at the corners on a plate well past the usual 100mm square. The slight sheen gives parts a clean machined appearance once tuned, and reviewers point to its suitability for 500-part production runs and technical components, which is a meaningful claim for anyone moving from one-off prototypes to batch work.
Mechanically it is a proper engineering choice: improved heat resistance over standard PETG, plus better wear, tensile and impact resistance, with reduced warping and better dimensional accuracy. For a slider, a wear surface or a component with moving contact, that combination is the point of the material rather than the colour.
Three requirements repeat across the reviews. Print speed has to come down for the best results, the filament must be dried thoroughly beforehand, and you should start with a fresh hardened steel nozzle. Once those are in place the layer lines become near invisible and parts hold up well in service.
Who this spool suits
Batch production and technical components where a clogged nozzle or a lifted corner would cost you more time than the material. It is also the safest carbon fiber choice for a first attempt because it is the least demanding of the group to feed.
What to watch for
Throughput drops if you print fast, so measure your real cycle time before planning a run. Fit a fresh hardened nozzle and dry the spool, and treat the reduced warping as a genuine benefit for large flat functional parts.
12. ELEGOO PETG Black – Budget Pick for Budget Brackets and Printer Upgrades
ELEGOO PETG 3D Printer Filament 1.75mm Black 1KG
1.75mm diameter
1kg spool
Plus or minus 0.02mm accuracy
Pre-dried and vacuum sealed
Wide FDM printer compatibility
Pros
- Excellent layer adhesion and strong finished parts
- Smooth clog-free extrusion with accurate diameter
- Neatly wound and tangle free out of the box
- Colours match the listing
Cons
- Noticeably glossy finish
- Retraction and temperature tuning needed to limit stringing
- Best results after re-drying once opened
This is the spool I keep on the shelf for the jobs that do not need expensive material. Printer upgrade brackets, cable guides, dust covers and mounting plates, all of it printed on the same settings without fussy calibration. Layer adhesion is genuinely good for the tier, and the 0.02mm accuracy claim is consistent with what came out of the extruder on my test parts.
Extrusion was smooth and clog-free across everything I printed, which is the main reason it earns a place on a functional bench. It arrives pre-dried and vacuum sealed, so a fresh spool is usually printable straight away, and the winding is neat enough that you get no tangles out of the box.
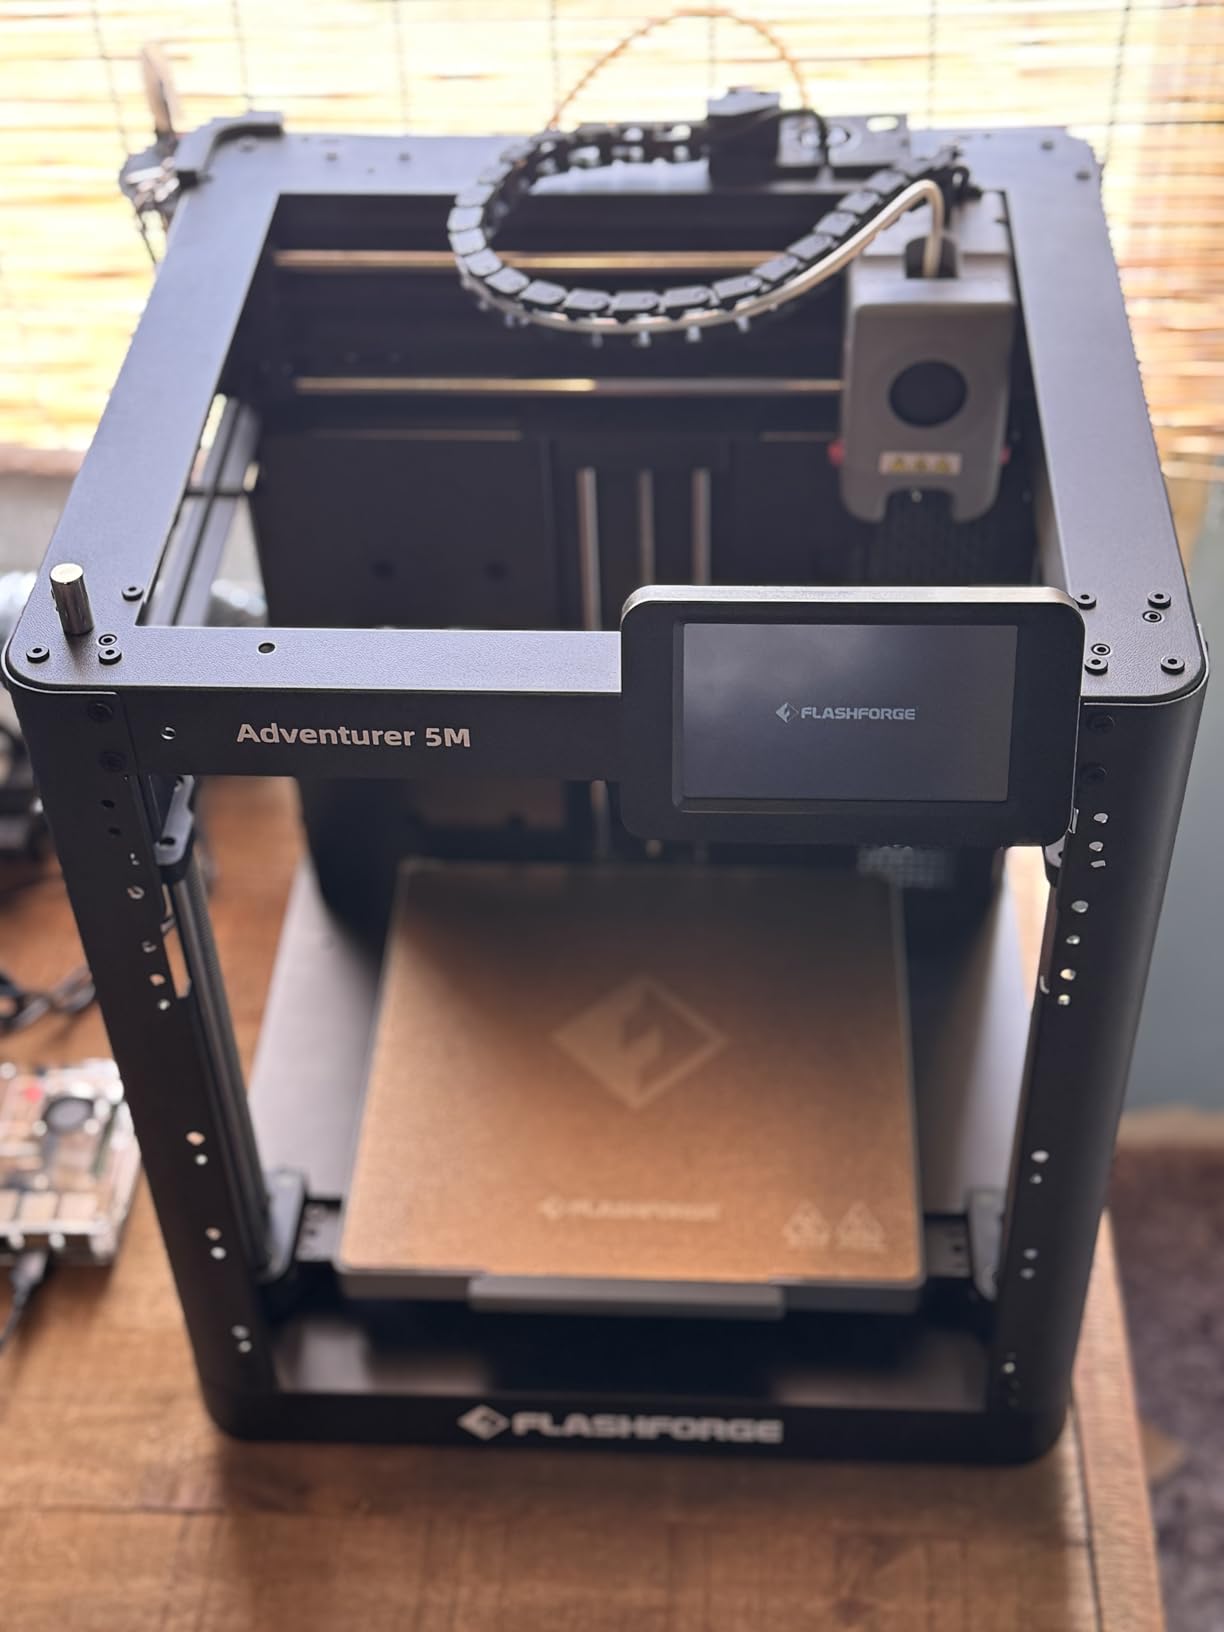
It is explicitly designed for mechanical parts, holders, clamps and printer components, and users confirm it delivers more durability than PLA for outdoor assemblies. Compatibility is broad across Neptune, Ender, Adventurer and Kobra machines, and the colours match the listing rather than running lighter than photographed.
The criticism that shows up most often is the finish. It is noticeably glossy, so it will not satisfy a matte-first brief, and it still needs retraction and temperature tuning to keep stringing under control on longer prints. Re-drying after the spool has been opened is worth doing if it has been sitting in open air.
Who this spool suits
High-volume functional printing, where the tolerance has to be dependable rather than exceptional and the material is a minor line item on the job. Brackets, clamps, spool holders and printer mods are the sweet spot.
What to watch for
Tune retraction and temperature once and save the profile, because the gloss plus stringing combination is what prompts most complaints. It is standard PETG, so it will soften earlier than the PETG-CF spools if a part lives somewhere hot.
How to Choose PETG Filament for Functional Parts
Choose by the load path in the part, not by the strength number. A bracket that carries a static load wants stiffness and interlayer strength, a clip or latch wants toughness and elongation, and a part that will be handled wants impact resistance. The sections below cover the decisions that actually change the outcome of a print.
What actually makes PETG strong in a functional part
Layer adhesion beats raw tensile strength, because a printed part is a stack of bonded sheets. Glycol modification is what allows polymer chains to diffuse across the layer interface while the previous layer is still warm, producing an interlayer bond strong enough that most PETG parts break in the bulk material rather than along a layer line. That is also why a part flexing more than you expected is not automatically bad filament; PETG is a flexible, tough material, not a rigid engineering plastic.
Two settings move layer adhesion more than any brand choice. Cooling fan percentage is the first lever, because over-cooling a layer before the next one lands starves the bond, and extrusion temperature is the second, since a higher nozzle temperature keeps the interface molten for longer. If you have one setting to change after moving to a new spool, change the fan.
Standard, high-flow, toughened or carbon fiber PETG
Standard PETG prints at 230-260C with little fuss and is the right answer for most functional work. High-flow formulations such as the Polymaker spool here are engineered for higher volumetric flow, so you can print faster without underextruding, which matters more than speed on a bracket. Carbon fiber PETG adds stiffness and heat resistance, and it changes the hardware requirements rather than the difficulty: hardened steel nozzle, sometimes a bigger bore, sometimes an enclosure.
Choose carbon fiber when the part must hold a shape under static load or live somewhere warm. Choose standard or high-flow PETG when the part flexes, clips, absorbs impact or has to survive being dropped. The honest trade-off is that carbon fiber raises stiffness and lowers toughness, so a rigid carbon fiber part can shatter on a hard knock where plain PETG would bend and survive.
Diameter tolerance and why it decides fit
Diameter tolerance is the spec most likely to decide whether an assembly works, and it is a different question from strength. A claimed plus or minus 0.02mm is the tightest in this group, and a plus or minus 0.03mm spool will still hold a press fit, but you may want to ream a hole or nudge your slicer compensation. Prusament stands apart because the figure is guaranteed and you can read the measured data for the specific spool by scanning its QR code, which is the closest thing to batch-level traceability in this list.
Ovality matters as much as the number. A filament that is round and consistent feeds predictably; one with variable ovality shows up as inconsistent extrusion and visible banding, which no temperature change will fix.
How to dry PETG and stop the stringing
PETG is hygroscopic, so it absorbs moisture from the air, and moisture is the root cause of most PETG complaints: stringing, popping, bubbles, rough surfaces and reduced layer adhesion. The numbers across the spools here point to one protocol: 55-65C for 4-6 hours for standard grades, up to 8 hours for carbon fiber blends, with container humidity kept below 20 percent RH.
Order the fixes by cause rather than by habit. Dry the filament first, because a damp spool will string no matter what you change. Then drop the nozzle temperature a few degrees within the recommended window, raise travel speed and add a small amount of extra retraction. Combing or wiping at travel helps the surface but does nothing for the underlying cause, which is water in the melt.
Keeping PETG from tearing your build plate
PETG bonds chemically to smooth PEI, and part removal can lift the plate coating with it. The sequence that helps is to score a gentle line on the print footprint with an old nozzle, keep the bed within the spool’s recommended range, and treat the plate with a thin layer of glue stick or an adhesive release agent to break the chemical bond. Never print a functional part straight onto clean smooth PEI if you intend to remove it, and let the bed cool fully before pulling.
The other warning is geometry. A first layer that is too hot or too squashed gives an elephant foot that welds itself to the plate, so a small Z offset and a modest first-layer temperature usually solve what looks like a plate problem.
Where PETG is the wrong choice
PETG is the wrong material in four situations. Sustained heat above roughly 80C will soften it, so a hot-end shroud or a part near an exhaust manifold is better in ASA or a carbon fiber filled grade with a higher deflection figure. Stiffness-critical geometry under constant load can creep, so keep the load path on the walls of the part rather than across a flat top surface.
Food and drink contact is another. Standard PETG is not certified for it, and a printed surface has layer lines that harbour residue. Constant UV exposure outdoors is the third, because prolonged sunlight degrades the polymer and ASA is the better outdoor choice.
None of these rule PETG out for a functional part; they tell you which part of the property curve you are trading away.
Frequently Asked Questions
What is the best filament for functional parts?
PETG is the best filament for most functional parts because of its layer adhesion and impact toughness, not its raw tensile strength. Glycol modification lets polymer chains bond across the layer interface, so a printed bracket fails in the bulk material rather than splitting along a seam. PLA is stiffer but brittle; ABS and ASA resist heat better but are harder to print and warp more.
Which brand of PETG filament is the strongest?
Strength comes in two forms and the answer differs for each. For stiffness and heat resistance among the spools we tested, FLASHFORGE PETG-CF rated highest at 4.8, followed by CC3D and Polymaker Fiberon PETG-rCF08. For dependable standard PETG, OVERTURE leads on review volume with more than 16000 reviews, and Prusament offers the tightest guaranteed tolerance at plus or minus 0.02mm.
Is PLA+ as strong as PETG?
PLA+ is stiffer than PETG and holds its shape better, but it is still brittle and will crack rather than flex. PETG absorbs impact and repeated bending without splitting, which is why it is the default for clips, latches, tool handles and brackets that get handled. For a stiff static load, PLA+ can be sufficient; for anything dropped, assembled repeatedly or exposed to a wrench, choose PETG.
Why do people hate PETG filament?
Most PETG criticism comes down to three behaviours. It strings more than PLA, because moisture in the melt causes it. It bonds to smooth PEI build plates so aggressively that removing a part can damage the coating. And it is hygroscopic, so an open spool degrades within days unless it is dried and stored sealed. All three are fixable with a drying routine, a release agent and a slightly lower nozzle temperature.
Is it possible to overdry PETG?
It is possible but rarely a problem. Drying too long at too high a temperature can embrittle the filament slightly or degrade additives, so keep to the 55-65C range for 4-6 hours on standard grades and up to 8 hours for carbon fiber blends. You will not ruin a spool by an extra hour, and filament that has been under-dried is far more common than filament that has been over-dried.
Is PETG ok to drink out of, and is it food safe?
Not as a default. Standard PETG filament is not certified for food contact in the way some manufacturers imply, and a printed surface carries layer lines that trap residue and are hard to clean. For a drinking vessel or anything that touches food repeatedly, use a filament that carries explicit food-contact certification and print with an all-around wall thickness, or choose a purpose-made material for the job.
The Best PETG Filament for Functional Parts in 2026
OVERTURE High Speed PETG is the best PETG filament for functional parts in 2026 because it is the only spool here that combines a 300mm/s ceiling, a claimed 0.02mm tolerance, AMS-friendly winding and vacuum-sealed packaging, with more than 16,000 reviews behind it. If your work is mostly brackets, clips and enclosures printed on a fast machine, that is the spool to start with.
For stiffness, FLASHFORGE PETG-CF is the pick, with the highest rating in the group and the cleanest feeding of the carbon fiber group. ANYCUBIC PETG-CF covers outdoor and weather-exposed parts, IEMAI PETG-CF does the same job on an open-frame printer, and Polymaker Fiberon PETG-rCF08 is the one with a published heat deflection figure. Prusament is the choice when tolerance is the deciding factor, Polymaker High Speed is the choice when throughput is, and ELEGOO is the choice when you are printing a hundred brackets and the material cost has to stay small.
Whatever you pick, dry it before the first print. That single step fixes more PETG problems than any brand change.